

Should the Core Be Annealed After Stamping?
Every stamped core loses a few percent to the punch, and a furnace can take some of it back. Annealing after stamping is a money question, since the punch adds loss and the furnace returns part of it. Jiangsu Zhongtong Weiye Special Steel Co., Ltd. runs that sum below, using a non-oriented electrical steel sheet as the example.
The Short Answer
Thin gauges, narrow limbs, and tight guarantees justify a furnace cycle, since three conditions push the same way. Thick gauges, wide limbs, and price driven orders rarely do. The gain runs near 5 to 10 percent of the material figure, while the cost runs a cycle plus distortion. Hence the answer depends on mass and duty, rather than on principle. The stress note covers the mechanism.
What the Punch Takes Away
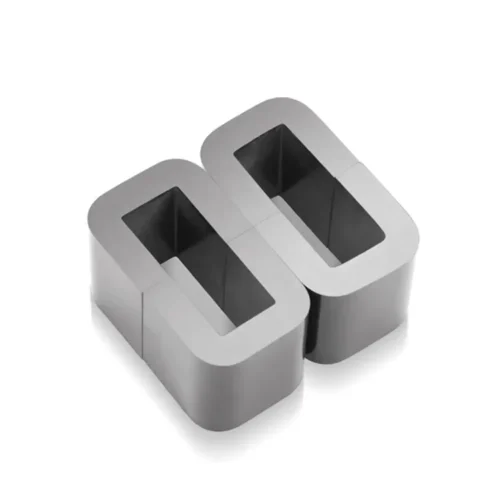
Shearing distorts the lattice within a few millimetres of each cut edge. That band carries higher loss, as the shear note explains. A narrow limb suffers more, because the edge band covers a larger share of its width. A core built from many small pieces therefore pays more than one built from a few large pieces. Hence geometry sets the size of the prize, not the grade.
What the Furnace Gives Back
A cycle near 750 to 800 degrees lets the lattice recover, so loss falls towards the parent figure. That window sits inside the heat limit. That recovery stays partial, because recrystallisation would need more heat than a relief cycle allows. Running hotter than 850 degrees starts grain growth and shifts the texture, so the magnetic result suffers. Therefore, the window is narrow, and it needs a controlled furnace.
The Sum in Watts and Euros
Take a 0.85 W/kg grade and add 10 percent for punching, so the core starts near 0.94 W/kg. A relief cycle brings it back to about 0.88, which saves 0.055 W/kg per unit mass. On 1.2 tonnes that reaches 72 W, since mass multiplies the gap. A cut core of that size is the usual case. At a capitalisation rate near 14 euros per watt, the saving is roughly 1,008 euros per unit. Hence the arithmetic stays short, while the decision turns on the four costs below.
What the Cycle Costs
A furnace cycle carries four costs, and each one bites somewhere. The heat costs energy, labour, and furnace time. Distortion costs flatness, because a stack relaxes and warps unless clamped, and it can cost coating as well. Coating costs insulation, since resin films cannot survive that temperature. Delivery costs weeks, because the furnace sits in a queue. Therefore, the saving must clear all four, and small units rarely clear two.
Three Cases That Decide It
A distribution unit with a tight no-load guarantee usually earns the cycle, since those watts are capitalised. Thick strip in a large power unit earns less, because the edge share is small and core losses dominate. A price driven order for a small unit rarely qualifies, since the queue outruns the saving. Hence the case list is short, and it fits on one page.
Recovery Is Not Recrystallisation
Two outcomes hide behind the word anneal, and only one belongs here. Recovery lets distorted grains relax in place, and it restores loss without changing the microstructure. Recrystallisation grows new grains, and it would ruin a texture that the mill spent a whole line building. A relief cycle aims at the first outcome, so the temperature stays low on purpose. Hence a hotter furnace is not a better furnace.
Batch or Continuous
Two furnace types serve two production rhythms, and they differ in distortion. A batch furnace loads a stack, soaks it, and cools it slowly, and it suits low volume with careful clamping. A continuous line carries strip through zones, and it suits coils rather than stacks. Hence the choice follows the product form, since a wound core never fits a continuous line.
What Goes Wrong
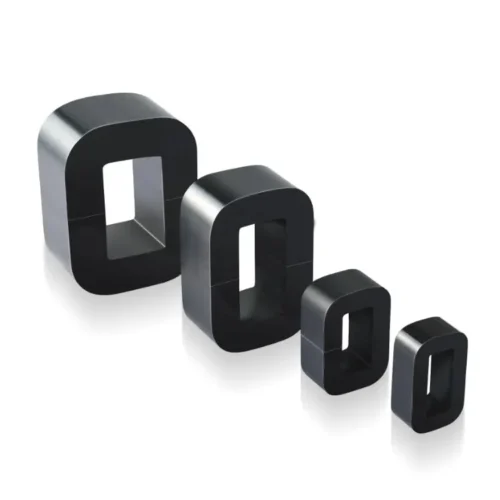
One buyer anneals a resin coated core, then finds insulation gone. Another anneals without a clamp, so the stack warps and the build fails. A third anneals a thick gauge core, where the gain never covers freight. Those three errors arrive monthly.
What We Do Not Do
We do not melt or roll steel. We do not run a furnace for a customer’s core, because that cycle belongs to the stamper. Nor do we promise a recovery figure without the grade and geometry.
Those limits keep the answer honest, and they keep a sum honest too.
Specify Your Order
Give the grade, the edge share, the mass, and the guarantee. Those four fields then price the cycle. Add the coating family, because a resin film forbids the furnace. A grain oriented sheet covers a different duty. A CRGO coil arrives when the core is wound. That reply usually takes a day.
Related Reading
Our cycle note covers how the furnace runs. The loss note separates the terms. A hub page answers six basic questions.
Frequently Asked Questions
About 0.05 W/kg, on a 10 percent punching penalty.
750 to 800 degrees, and never above 850, since grain growth starts there.
To hold flatness while the metal relaxes, and to keep the build.
No, since the film breaks down near 180 degrees, far below the cycle.
No, since thick strip earns less than thin, and the edge share shrinks.
- Email: vera.liang@ztwysteel.com
- Location: Xishan District, Wuxi, Jiangsu, China
- Supply range: CRGO and CRNGO 0.20–0.65 mm, four coating classes
- Slitting: 20–1,250 mm, ±0.05 mm, burr under 0.02 mm
- Documentation: MTC EN 10204 3.1 with grade, thickness and loss basis, 3.2 on request





 English