

Yield Strength of Silicon Steel Sheets
A stamping shop cracks a lamination, and the first question is always the yield figure. Yield strength of silicon steel rarely answers that crack, since a die needs elongation and edge quality. Jiangsu Zhongtong Weiye Special Steel Co., Ltd. quotes the mechanical values on the silicon steel sheet certificate, so the paper matches the coil.
The Short Answer
An annealed 0.50 mm non-oriented sheet lands near 300 to 380 MPa at 0.2 percent offset, with 450 MPa tensile. A grain-oriented sheet runs a little higher, near 350 to 420 MPa, and breaks sooner across the roll. Hence the number exists, and the crack usually comes from somewhere else.
Why the Curve Looks Odd
Electrical steel holds almost no carbon, so a sharp upper yield point often fails to appear. The curve bends over instead, and the 0.2 percent offset becomes the working definition. Some heats show a short yield elongation, since a trace of carbon and nitrogen remains. Therefore, a report should name the offset, or the figures cannot be compared.
What Silicon Does to Yield
Silicon sits in solid solution, and each addition pins dislocation motion, so yield climbs with the alloy. A 3 percent grade then sits above a 0.5 percent grade at the same grain size. That gain costs ductility, since the same pinning limits slip. Hence a higher silicon grade stamps harder and cracks sooner.
What the Anneal Does
Recrystallisation wipes out the dislocation density from cold rolling, so a full anneal pulls yield to its floor. A partial anneal leaves some cold work in place, and the yield then sits higher by tens of MPa. A buyer who compares two coils should check the anneal, not just the grade. Therefore, the thermal history moves the number more than the chemistry.
What Grain Size Does
Finer grains raise yield, since more boundaries block slip, and the effect follows a square-root law. Mills that hold a coarse grain for low loss then ship a softer sheet. Fine-grain heats lose magnetic quality and gain strength. Hence the magnet and the press pull in opposite directions.
Three Numbers That Get Mixed
Tensile strength sits about 150 MPa above the yield, and a buyer who quotes it as yield oversizes a press. Hardness reads the surface resistance, and it tracks tensile strength rather than yield. The 0.2 percent offset value differs from a lower yield point on a curve with a plateau. Therefore, three numbers, three meanings, one label on the drawing.
What the Die Really Needs
Press tonnage follows yield and sheared area, so a 10 mm2 section at 300 MPa needs near 3 kN. Edge quality follows elongation and clearance, since a brittle sheet tears where a ductile one shears clean. Die wear follows hardness and coating. Hence the drawing should carry all three, not one.
What the Coating Changes
A coating a few microns thick barely moves a static yield, since the metal carries the load. It does change friction in the die, and friction changes the punch load. A rough coating raises the stripping force and the wear. Therefore, the film matters to the press, not to the tensile bar.

What Temperature Changes
Yield falls a little as the sheet warms, so a warm coil stamps easier than a cold one. The change stays small below 100 °C. A hot stamping line may gain a few percent in formability, and that gain is not a grade change. Hence the shop should hold the coil at one temperature for a fair comparison.
Where the Numbers Come From
A tensile test follows ISO 6892-1 or ASTM E8, with an 80 mm gauge and a transverse specimen. Mills report Rp0.2, Rm, and A80 on a non-oriented sheet, since each one needs its own note. Buyers who ask only for yield force the mill to guess. Therefore, ask for the trio and the test standard.
Where the Crack Really Starts
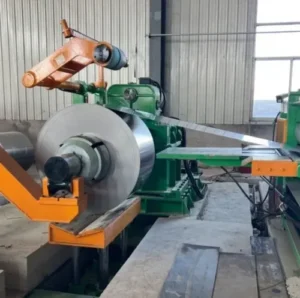
Burs above 0.02 mm concentrate strain, so the crack starts at the edge rather than in the metal. Tight die clearance tears a brittle sheet at the corner. Slitting lines that work-harden the edge raise local yield, and that edge fails first. Hence the edge condition outranks the bulk figure.
Where Buyers Get It Wrong
A buyer specifies yield alone and ignores elongation. Another compares a partially annealed coil with a fully annealed one. A third reads hardness as yield. Those three errors cover most of our returns.
What We Do Not Do
We do not melt, roll, or anneal steel. We do not run a tensile test in house. Nor do we restate a mill value under a different offset.
Those limits keep the answer honest.
Specify Your Order
First, give the grade and the thickness. Second, ask for Rp0.2, Rm, and A80 with the test standard. Then state the die clearance, so the edge condition enters the discussion.
Related Reading
The grade naming note explains the loss code, so a 50W470 sits beside a 23P85. The chemistry note covers the alloy side, which sets the strength floor.
Frequently Asked Questions
What is the yield of a 0.5 mm sheet? Near 300 to 380 MPa at 0.2 percent offset.
Does silicon raise yield? Yes, since it pins dislocation motion.
Why no sharp yield point? Carbon is too low to form a clear plateau.
Which value should a die use? Yield for tonnage, elongation for edge quality.
Does the coating change yield? Barely, though it changes die friction.
- Email: vera.liang@ztwysteel.com
- Location: Xishan District, Wuxi, Jiangsu, China
- Supply range: CRGO and CRNGO 0.23–0.65 mm, mechanical values on request
- Slitting: 20–1,250 mm, ±0.05 mm, burr under 0.02 mm
- Documentation: MTC EN 10204 3.1 with Rp0.2, Rm and A80, 3.2 on request





 English