

What Is Stacking Factor?
A core drawing shows a solid block, and the steel inside fills only part of it. Stacking factor is the ratio between the two, since coating, burr, and air take the rest. Jiangsu Zhongtong Weiye Special Steel Co., Ltd. follows that ratio in three directions below, starting from silicon steel sheet as the raw input.
The Short Answer
Stacking factor divides net steel area by gross area, and a typical value runs 0.95 to 0.97. That number is not a constant, because it falls as the strip thins. Three parties feel it, so three budgets carry the cost. Each party meets a different part of it.
Direction One — The Designer Multiplies
A designer who needs 100 cm² of steel must ask for about 104 cm² of envelope at 0.96. Net area equals gross area times the factor, so the envelope grows by the inverse. Skip that step and the core comes up short, which shows up as a hot winding. Hence a drawing needs the factor printed on it, rather than left to memory.
Direction Two — The Buyer Divides
Weight follows the net steel, so a gross volume times density overstates the mass by 4 percent. A limb of 200 mm by 200 mm over one metre holds 314 kg as a solid block. At 0.96 the steel inside weighs 301 kg, which leaves 13 kg of coating and air. Therefore, a drawing-based weight always runs high, and invoices follow the steel rather than the outline. Our weight calculation guide works through the same arithmetic, since the two questions share one formula.
The Hidden Third — Flux Density Climbs
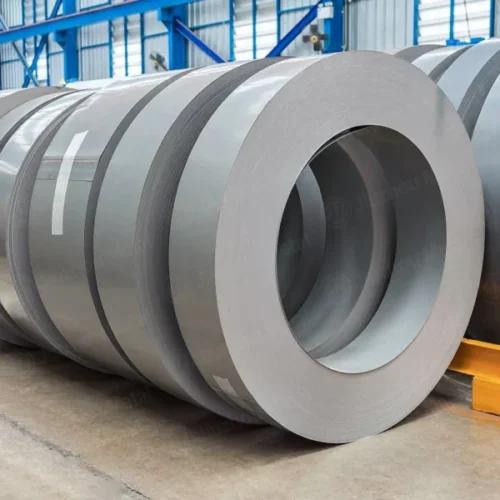
Flux is set by voltage, while area is what it divides into. Shrink the area by 4 percent and the flux density rises by the same share. That takes 1.5 T to 1.56 T, since the flux itself never moved. Loss climbs with the square of that figure, so the bill rises about 8 percent. Hence a small geometry error becomes a large thermal one.
Why the Number Falls as Strip Thins
Coating holds a fixed micron thickness, while the strip behind it shrinks. At 0.50 mm a 20 μm allowance covers both sides plus the gap. At 0.23 mm the same allowance eats a larger share, so the factor drops toward 0.94. Therefore, thin gauges pay a double penalty, once in coating share and once in useful area. A CRGO coil at 0.23 mm therefore carries less steel per cubic metre than a 0.50 mm coil.
What Moves the Number
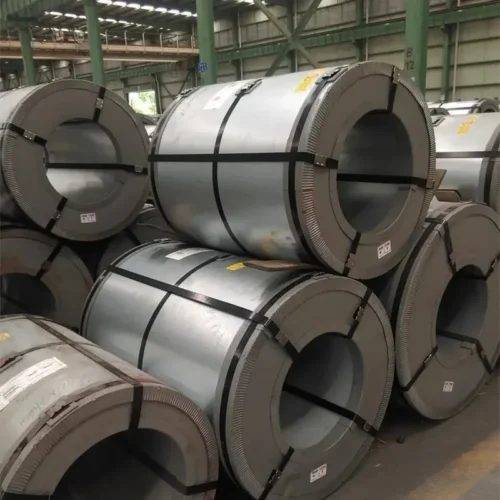
Four items shift the ratio, and each is visible on a coil. Coating class sets the film weight, since a C5 layer is heavier than a C3 one. A heavy film then eats area. Burr of 0.02 mm stands the sheets apart and lets air in. Roughness and camber add gap across a wide sheet, because a crowned strip never lies flat. Stacking pressure closes some of it, while a loosely clamped core reads low.
Not the Same as Building Factor
Building factor compares an assembled core with the Epstein strip, and it runs 1.1 to 1.3. Stacking factor is pure geometry and never touches the watts. A buyer who mixes the two predicts a loss that no test confirms. Therefore, keep the names apart on a spec sheet, since one is measured and one is weighed.
How to Check It
Weigh a stack, measure its envelope, and divide the two volumes. The result is the factor, and it needs no laboratory, because a scale settles the question. A silicon electrical steel sheet arrives with its coating class, so the check starts from a known film. Repeat on three stacks, since burr varies across a slit width. Hence a single weighing is not enough on a wide coil.
What Goes Wrong
One buyer prices a core from a drawing and finds the invoice 4 percent lighter. Another sizes a limb on gross area and blames the grade for a hot core. A third compares 0.96 with a building factor and expects a phantom saving. Those three errors arrive monthly, although each has a one-line cure, so none of them is expensive to avoid.
What We Do Not Do
We do not melt or roll steel. We do not design a customer’s core. Nor do we quote a stacking factor that no weigh check supports, since a guessed ratio misprices the coil.
Those limits keep the answer honest, and they keep the ratio measurable.
Specify Your Order
Give the gauge, the coating class, and the burr limit, since all three set the ratio. Add the stacking pressure when a core is clamped hard. A non-oriented sheet then arrives with a stated film weight, while a cut core covers assembled parts. That reply usually takes a day, since the answer needs only three fields.
Related Reading
The insulation note explains why the coating exists at all. Our hysteresis note covers the loss that a wrong area inflates. A hub page answers six basic questions.
Frequently Asked Questions
Yes, since both names describe one ratio.
About 0.96, though a heavy coating lowers it.
No, it changes the area you order.
Yes, by weighing a stack.
Coating holds a fixed thickness, so its share grows.
- Email: vera.liang@ztwysteel.com
- Location: Xishan District, Wuxi, Jiangsu, China
- Supply range: CRGO and CRNGO 0.20–0.65 mm, four coating classes
- Slitting: 20–1,250 mm, ±0.05 mm, burr under 0.02 mm
- Documentation: MTC EN 10204 3.1 with grade, thickness and loss basis, 3.2 on request




 English