Professional Insights into the Mechanical Strength of Tin-Plated Steel Coils
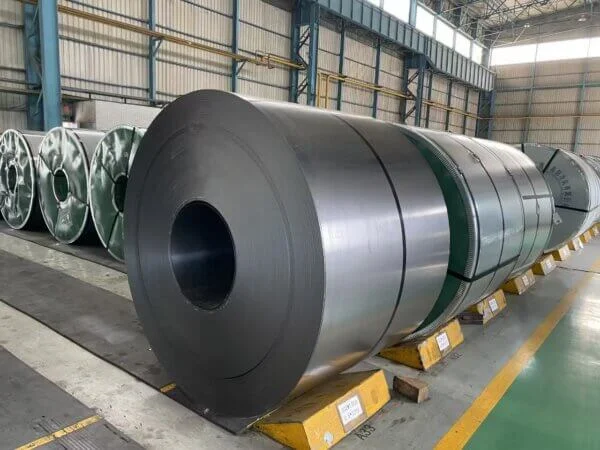
The mechanical strength of tin-plated steel coils comes almost entirely from the steel base, not the tin. The tin layer is only 0.2–0.8 microns thick; it does not contribute measurable tensile strength. Consequently, when buyers ask about strength, they are really asking about the temper of the underlying low-carbon steel. Here is what each test number means in practice.
Tensile Strength: The Number on the Mill Certificate
Tensile strength measures the maximum stress the steel withstands before breaking. For tinplate, it ranges by temper:
- T1–T2: 280–350 MPa. Soft, deep-drawable.
- T3–T4: 340–420 MPa. General-line cans.
- T5–T6: 400–500 MPa. Rigid battery cases and shallow draws.
- DR550–DR800: 550–800 MPa. Double-reduced, work-hardened, lightweight food cans.
Typically, buyers order by temper grade rather than tensile number, because the temper code already bundles strength, ductility, and hardness. However, if your stamping die has a specific spring-back requirement, ask for the actual MPa range on the MTC.
Yield Strength and the “Drawing Limit”
Yield strength tells you when the steel stops behaving elastically and starts deforming permanently. For deep-drawn cans, low yield is good—it means the steel flows evenly without local thinning. For DR cans, higher yield means you can use thinner gauge without buckling.
In practice, the yield-to-tensile ratio matters more than either number alone. A ratio below 0.6 indicates good deep-drawing behavior; above 0.75, the steel is stiff and resists forming.
Hardness: HR30T, Not Rockwell C
Tinplate is too thin for Rockwell C testing. Instead, mills report HR30T (Rockwell Superficial, 30 kgf load, T-scale). Typical values:
- T1–T2: 45–55 HR30T
- T3–T4: 55–65 HR30T
- T5–T6: 65–72 HR30T
- DR550+: 72–80 HR30T
This number correlates directly with your die wear rate. Harder temper means faster die wear, but thinner material.
Bend Test: Does It Crack on the Line?
The bend test (often a 180° reverse bend around a specified mandrel) checks ductility. Soft T2 should bend flat without cracking. Hard DR800 may crack on a tight radius; consequently, die designers must allow larger bend radii for high-tempers. Always specify the bend test requirement on your PO—otherwise, the mill ships to its own default.
What the Tin Coating Actually Affects
The tin does not change tensile strength, but it affects surface friction during forming. A smooth, oiled tin surface draws more consistently than bare steel. Furthermore, if the tin is too thick, it can smear during deep drawing and cause die pickup. For most can-making, 2.8/2.8 g/m² strikes the right balance.
Other Coil Products We Supply with Test Certificates
The same tensile/yield/hardness testing applies to the other coil and sheet products we ship:
- C72200 Copper Plate reports tensile and yield strength per ASTM B152 for corrosion-resistant copper-nickel-zinc applications.
- C22000 / H90 Brass Pipe comes with its own tensile and hardness data for plumbing and fitting use.
- M43 Non-Oriented Electrical Steel and 50W1300 Non-Oriented Electrical Steel ship with lamination stamping ductility data, because motor cores must punch cleanly without edge cracking.
Specify Strength as a Temper Code
A complete tinplate strength specification reads: “T3 temper, 0.20 mm, 2.8/2.8 g/m², HR30T target 58–62, 180° bend test around 0.20 mm mandrel.” Leave out the temper and you cannot predict stamping behavior.
Get the Right Coil for Your Forming Line
Tell us your end-use, forming process, and required temper. We will recommend the correct SR or DR grade and quote coil with a mill test certificate showing tensile, yield, hardness, and bend data.
- Email: vera.liang@ztwysteel.com
- Location: Xishan District, Wuxi, Jiangsu, China
- Supply range: electrical steel, copper & brass plate/pipe, nickel alloys, wear plate, mold steel
- Documentation: MTC with chemistry, tensile/yield, hardness, coating weight, and dimensional tolerance
We reply within one working day.


 English