Creating High-Quality Tin-Plated Substrates Using the Cold Rolling Process
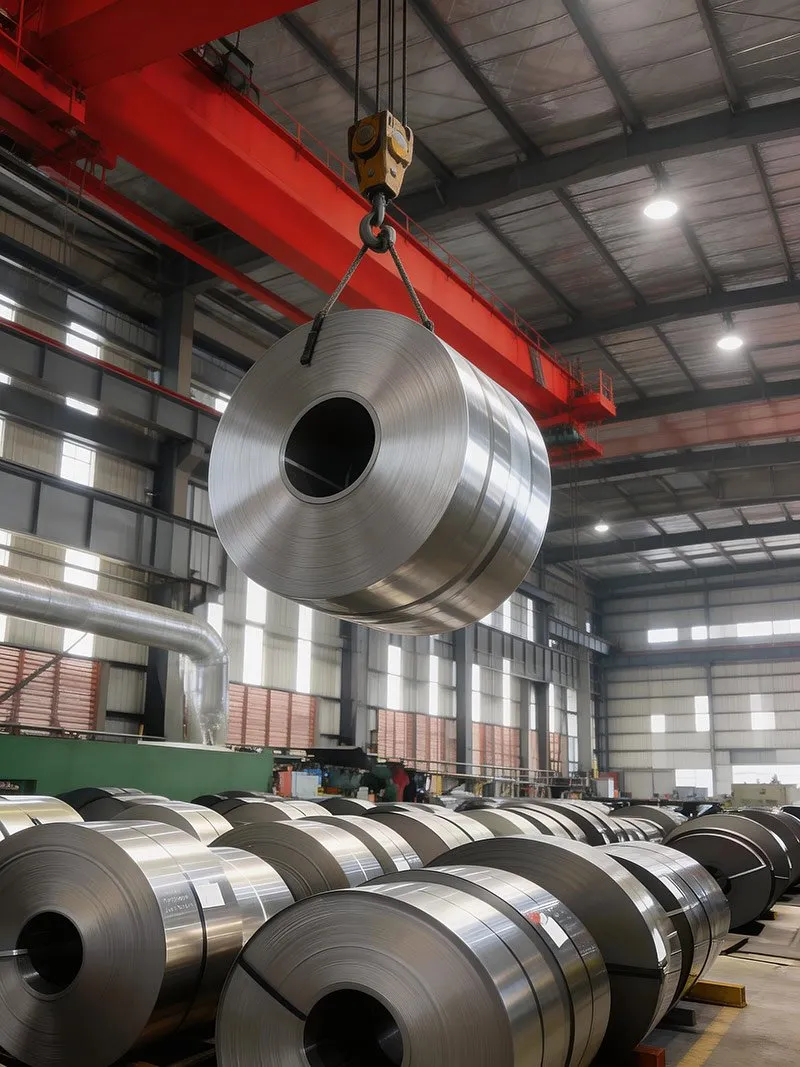
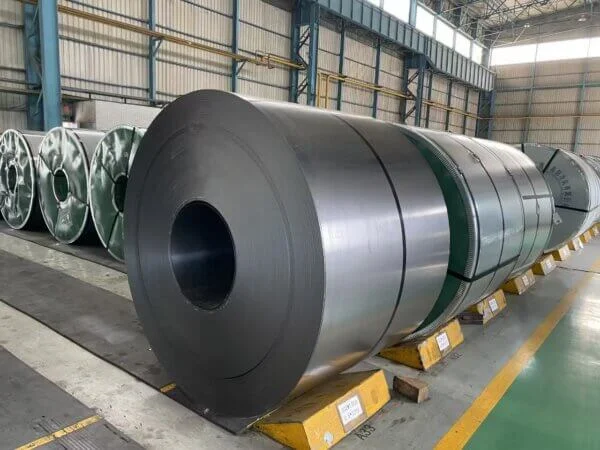
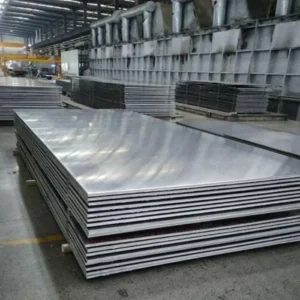
Cold rolled tinplate begins as hot-rolled steel coil, yet it ends as 0.15–0.50 mm strip within tight tolerance. Consequently, the cold rolling process decides thickness, flatness, and surface quality before tin is even applied. Here are the four key steps that transform hot band into can stock.
Step 1: Pickle and Cold Roll to Intermediate Gauge
First, the hot-rolled coil passes through an acid pickling line. This removes mill scale and oxide. Next, the cold mill reduces thickness in several passes. Typically, a 2.5 mm hot band rolls down to 0.5–1.5 mm intermediate gauge. Each pass reduces thickness by 30–50%. Furthermore, rolling work-hardens the steel, making it hard and brittle.
Step 2: Recrystallization Annealing
Consequently, after cold rolling the steel is too hard for can making. Therefore, it goes through batch or continuous annealing. At 600–700°C, the work-hardened structure recrystallizes. As a result, the steel softens and becomes formable. However, at this stage the surface is matte and unfinished.
Step 3: Temper Rolling (Skin Pass)
After annealing, the strip receives a final light reduction (0.5–3%). This temper roll does three things:
- Sets the final mechanical properties (T1 through T6 temper).
- Produces the desired surface finish (stone finish or bright finish).
- Flattens the strip for slitting and can making.
Furthermore, this step determines the can maker’s formability. Too hard and the can cracks; too soft and it wrinkles during forming.
Step 4: Tin Plating and Passivation
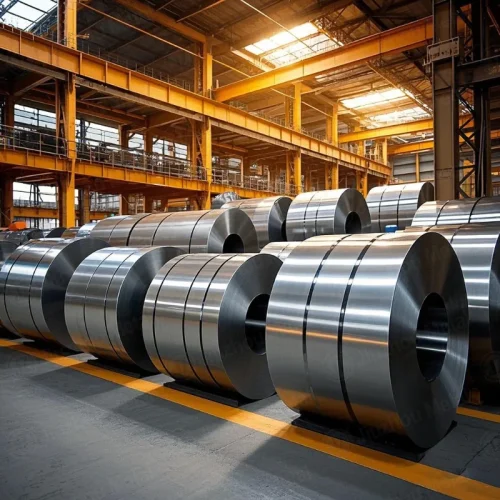
Finally, the cold-rolled substrate enters the electrolytic tinning line. Here, tin deposits at 1.1–11.2 g/m² per side. Then reflow melts the tin to produce a bright, reflective surface. Consequently, the cold rolling underneath is invisible, yet it controls the flatness and uniformity of the final product.
What Buyers Should Specify
A complete tinplate order reads: “T3 temper, 0.20 mm × 800 mm coil, 2.8/2.8 g/m², stone finish, palm oil 10 mg/m².” The temper designation (T1–T6) comes directly from temper rolling. Consequently, specify the temper, not just the thickness.
Related Cold-Rolled Substrates
Cold rolling logic applies beyond tinplate:
- C11000 / T2 Copper Plate arrives cold-rolled and annealed, with controlled flatness for busbar fabrication.
- C26800 / H65 Brass Strip gets cold-rolled to tight thickness tolerance for stamping terminals.
- C12200 / TP2 Copper Tube is cold-drawn to precise dimensions for refrigeration lines.
Source Cold-Rolled Substrates
Tell us your required thickness, temper, and width. We will confirm available stock and quote with a mill certificate.
- Email: vera.liang@ztwysteel.com
- Location: Xishan District, Wuxi, Jiangsu, China
- Supply range: cold-rolled copper plate/tube/strip, tinplate substrates, nickel alloys
- Documentation: MTC with thickness tolerance, temper, surface finish, and coating weight
We reply within one working day.

 English