Strictly Controlling the Metal Product Manufacturing Process: Advancing Enterprise Production Progress
Metal product manufacturing fails in predictable ways: wrong chemistry, missed heat treatment, hidden cracks. Consequently, process control is not paperwork—it is the difference between a part that lasts and a part that breaks. Here is how a disciplined shop controls each stage, from incoming material to shipping.
Stage 1: Incoming Material Inspection
Every shipment arrives with a mill test certificate (MTC). However, the certificate is not enough. The shop verifies:
- Chemistry against the purchase specification.
- Hardness on a Brinell or Rockwell tester.
- Dimensions with calipers and micrometers.
- Visual surface condition for cracks or laps.
Furthermore, for critical parts, the shop sends samples to an outside lab for spectrometer verification. If the material fails, it returns to the supplier. Consequently, bad steel never reaches the saw.
Stage 2: Sawing and Machining
After material approval, the shop cuts blanks on a bandsaw. Typically, it leaves 2–3 mm machining stock per side. Next, CNC mills and lathes bring parts to final dimensions. Consequently, the operator checks first-article dimensions before running a full batch. Furthermore, in-process checks every 10–20 parts catch tool wear before it causes scrap.
Stage 3: Heat Treatment
Heat treatment decides whether the part reaches its designed hardness. Typically, the shop sends parts to a certified heat treater that records:
- Austenitizing temperature and hold time.
- Quench medium and cooling rate.
- Tempering temperature and time.
Consequently, the heat treat report travels with the parts. If hardness is out of spec, the batch returns for re-heat treatment. However, re-heat treatment has limits—too many cycles cause grain growth.
Stage 4: Non-Destructive Testing
After heat treatment, critical parts get NDT:
- Ultrasonic testing detects internal cracks and inclusions.
- Magnetic particle testing finds surface cracks in ferrous parts.
- Dye penetrant testing reveals fine surface defects.
Furthermore, pressure vessels and structural parts also get tensile and impact tests. These destructive tests happen on witness coupons from the same heat.
Stage 5: Finishing and Surface Treatment
Finally, parts go through grinding, polishing, or coating. Typically, this removes tool marks and adds corrosion protection. Furthermore, the shop inspects surface roughness with a profilometer when the drawing specifies Ra. Consequently, parts leave the shop with a documented finish.
Stage 6: Final Documentation and Packing
Before shipping, the shop assembles the final packet:
- MTC from the mill.
- Heat treatment report.
- NDT report.
- Dimensional inspection report.
- Material traceability number.
Consequently, the customer can trace every part back to the original heat. This matters for aerospace, medical, and pressure vessel work.
Products We Supply as Controlled Stock
We apply the same discipline to the materials we ship:
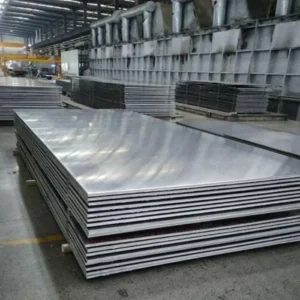
- Hastelloy C-276 Plate ships with MTC and PMI verification.
- H13 / SKD61 Mold Steel arrives soft-annealed with hardness test report.
- 400HB Wear Resistant Steel Plate ships with Brinell hardness certificate.
Get Controlled Material for Your Shop
Tell us your part, material spec, and required documentation. We will ship stock with a complete MTC packet.
- Email: vera.liang@ztwysteel.com
- Location: Xishan District, Wuxi, Jiangsu, China
- Supply range: nickel alloys, mold steel, wear plate, copper, electrical steel
- Documentation: MTC, heat treatment report, NDT, dimensional inspection
- Traceability: heat number on every plate and bar
We reply within one working day.

 English