Spot Welding Operation Guide for Silicon Steel Sheets
Setembro 14, 2026
Blogue
I. Analysis of Difficulties in Silicon Steel Sheet Spot Welding
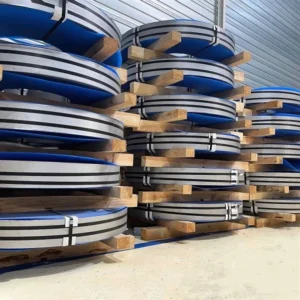
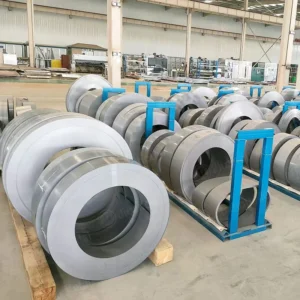
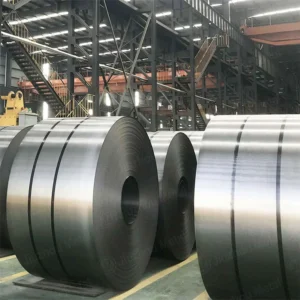
Aço ao silício sheets are difficult to weld due to the insulating coating on their surfaces that obstructs tight metal contact. Three typical defects frequently occur during spot welding:
- Weak weld joints: The coating creates excessive contact resistance and hinders heat conduction.
- Blackened weld spots: Improper current parameters trigger surface oxidation.
- Severe electrode sticking: Insufficient electrode pressure causes the material to adhere to electrodes.
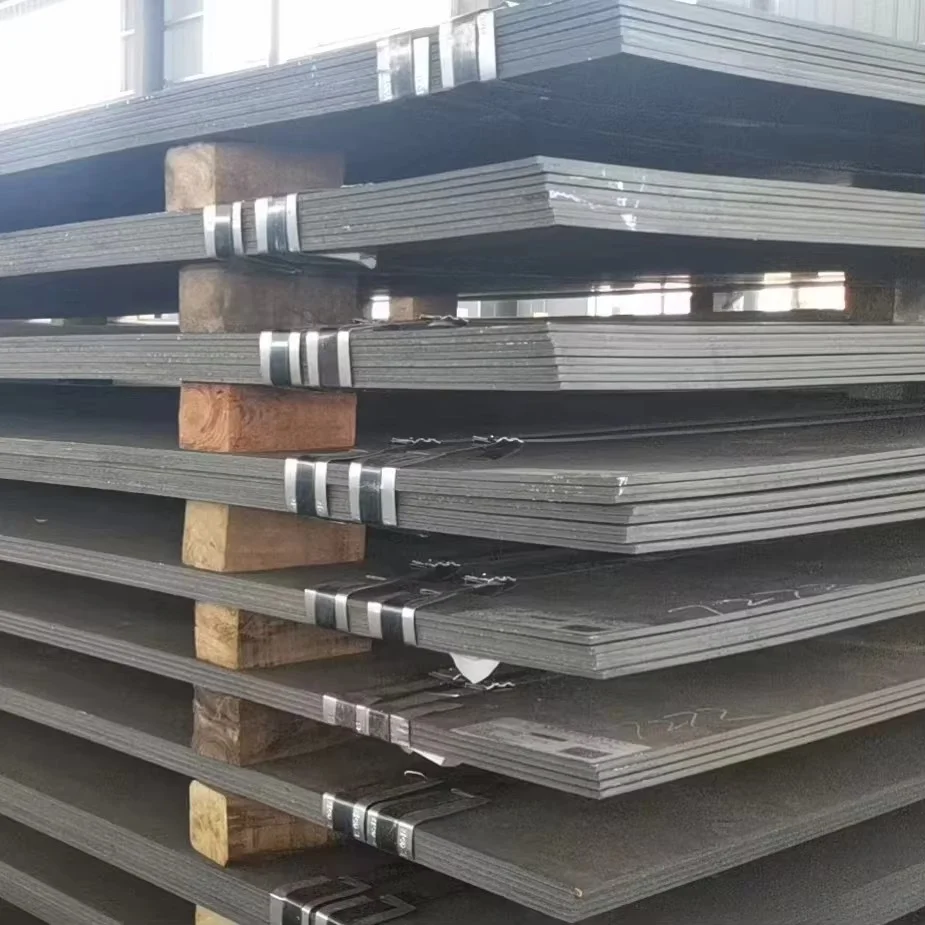
II. Four Steps to Achieve Flawless Weld Spots
Following this standardized procedure delivers immediate improvements in weld quality:
- Equipment selection: Secondary rectifier welders are recommended; AC welders are prone to magnetic blow.
- Optimized parameter matching: Increase welding current by 15%–20% compared with ordinary steel sheets and reduce energization time by 30%.
- Electrode preparation: Adopt chromium-zirconium copper electrodes with an end face diameter of 3–5 mm.
- Pressure control technique: Apply pre-pressure for 0.5 seconds before energization, and maintain pressure at 3–5 kgf/mm².
III. Minor Practices to Extend Equipment Service Life
These easily overlooked operating routines are critical for equipment maintenance:
- Gently polish electrode surfaces with fine sandpaper before daily startup.
- Check electrode concentricity every 500 welds; rework electrodes if deviation exceeds 0.2 mm.
- Release electrode pressure if the welder will be idle for more than 2 hours.
- Maintain cooling water temperature between 20–30 °C; higher temperatures accelerate electrode oxidation.


 English
 Japanese
 Korean
 French
 German
 Spanish
 Portuguese
 Russian
 Arabic
 Italian
 Turkish
 Dutch
 Polish
 Swedish
 Danish
 Norwegian
 Finnish
 Greek
 Hungarian
 Czech
 Romanian
 Bulgarian
 Slovenian
 Croatian
 Slovak
 Malay
 Indonesian
 Thai
 Vietnamese
 Myanmar
 Khmer
 Lao
 Tagalog
 Hindi
 Bengali
 Urdu
 Nepali
 Sinhala
 Hebrew
 Ukrainian
 Serbian
 Icelandic
 Swahili